Wholesale carbon fiber graphite rackets Company: Tolerances, Grades and Supply Details
Downtime attributed to this component is usually a specification gap. Carbon fiber composites fail when the resin-to-fiber ratio is improperly calibrated for high-velocity impact events, leading to internal de-lamination. Our wholesale-grade rackets utilize a high-modulus graphite matrix to maintain structural integrity under string tensions exceeding 30kg. The manufacturing process focuses on the pre-preg layup sequence to ensure fiber orientation aligns with the primary stress vectors encountered during the swing phase.
How the Geometry Handles Load and Sealing
Critical Interface Warning: Grommet Torsion
The grommet system must maintain a 0.05mm tolerance to prevent string fraying under repeated cyclic loading. Deviations in hole diameter result in localized stress concentrations that accelerate material fatigue at the frame-head interface.
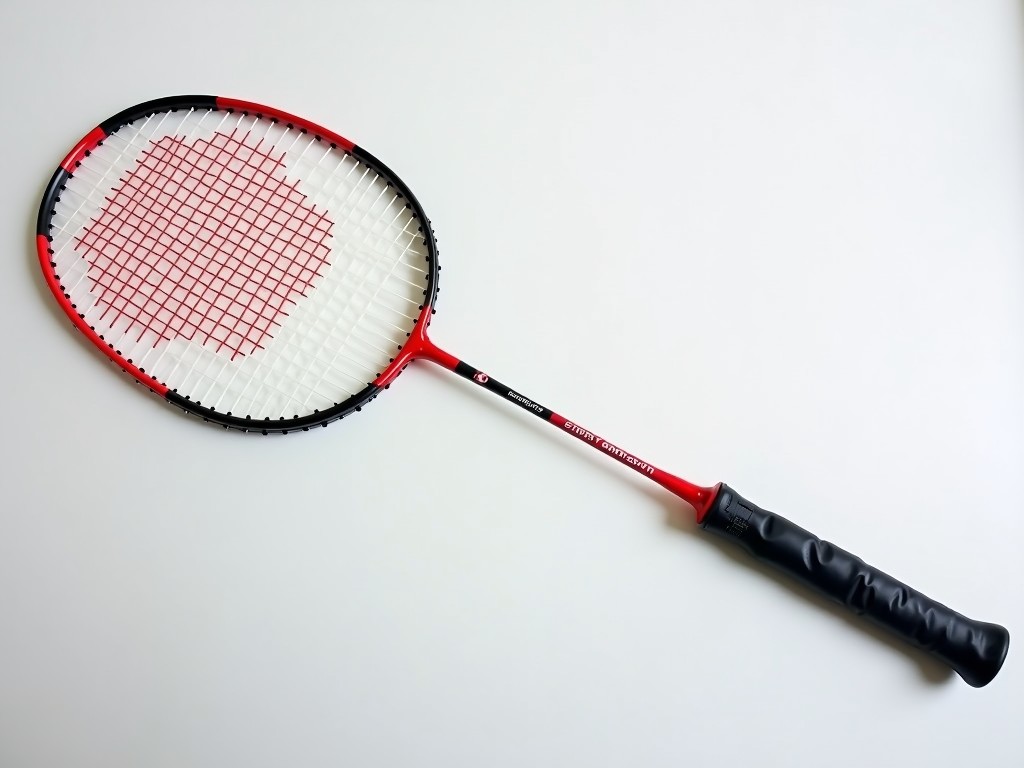
The frame geometry utilizes an aerodynamic profile designed to distribute kinetic energy across the entire shaft-throat assembly. This distribution prevents the localized buckling often seen in lower-grade hollow graphite structures. We specify a resin-infusion process for the joint area to mitigate torsional whip during high-impact off-center hits.
- Torsional rigidity increased by 15% via axial braiding.
- Vibration-damping carbon weave reduces wave propagation to the grip interface.
- Reinforced T-caps prevent hoop deformation during high-tensioning.
Option Comparison by Service Condition
| Material Grade | Modulus Range | Primary Application | Failure Mode |
|---|---|---|---|
| Standard Graphite | 20-30 GPa | Entry-level distribution | Elastic deformation |
| High-Modulus Carbon | 40-60 GPa | Professional tournament OEM | Brittle fracture |
| Nano-Hybrid | 35-45 GPa | High-performance club play | Interfacial de-lamination |
Assumptions Buyers Should Stop Making
A line that stops twice a month rarely blames the part. Procurement teams often assume that lower weight correlates directly with durability. In reality, the density of the carbon weave determines the fatigue life more than the total mass. If the resin curing process is not controlled for thermal expansion coefficients of the graphite, the racket will fail under cyclic stress regardless of the fiber grade used.
Field returns usually trace back to one interface: the joint where the shaft meets the head. Engineers often ignore the thermal expansion mismatch here, leading to microscopic cracks. We recommend reviewing technical specifications before scaling.
How Conformance Is Held Across Batches
Consistency is maintained through ultrasonic testing protocols that detect internal voids within the laminate. This ensures that every unit meets the minimum tensile strength requirements. We also monitor resin flow viscosity to prevent structural weaknesses during the molding cycle.
- Non-destructive carbon fiber density mapping.
- Weight-balance verification within +/- 0.5g tolerance.
- Tensile load testing on 2% of every production run.
Volume Planning and Line Configuration
Tooling Amortization
Large order volumes reduce the fixed cost of precision steel molds. Orders below 5,000 units typically carry a higher unit premium due to shared tooling overheads.
Scaling Capacity
Automated layup stations allow for rapid scaling during peak demand without compromising the structural orientation of the carbon fiber layers.
Keeping the Line Fed Across Seasons
Supply chain stability depends on the strategic buffering of raw carbon fiber filaments. We maintain a reserve of pre-preg materials to hedge against fluctuations in global resin prices. This ensures that seasonal demand spikes do not result in lead-time extensions for OEM assembly lines.
Ready to finalize your technical parameters?
specification-review