Specifying Pickleball paddle designs Factory for Industrial Service
Field returns usually trace back to one interface where the carbon fiber composite face meets the polymer honeycomb core. In high-volume production, the consistency of the adhesive bond line determines the long-term fatigue resistance of the paddle under cyclic loading. Engineers prioritize a uniform core-thickness tolerance of ±0.2mm across the striking surface to prevent uneven stress distribution that leads to structural delamination.
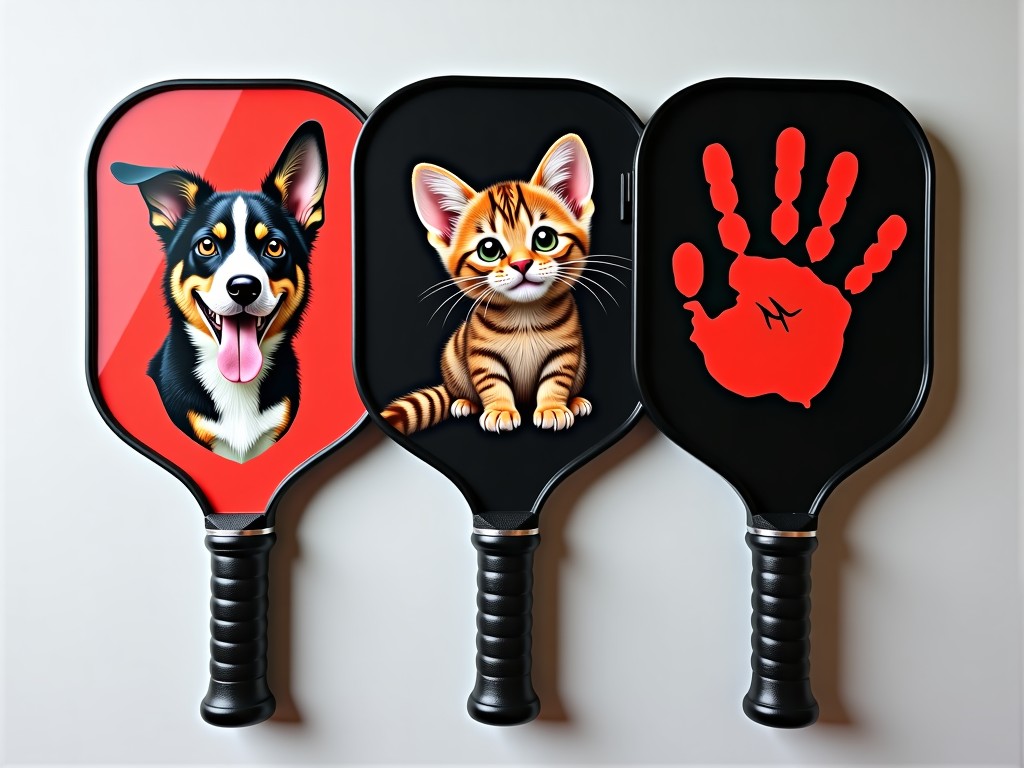
Downtime attributed to this component is usually a specification gap regarding the modulus of the resin system used. When sourcing for wholesale "funny" designs, the technical challenge shifts to ensuring the adhesion of UV-printed graphics on textured carbon fiber surfaces without compromising the structural integrity of the substrate. Lower-grade resins often fail to account for the thermal expansion cycles common in outdoor play environments.
What This Component Does in Service
Energy Transfer
The honeycomb core density dictates the coefficient of restitution. Higher-density cores minimize energy loss during the impact compression period.
Vibration Damping
Internal cell walls absorb high-frequency oscillations, reducing mechanical stress on the end-user during repetitive stroke cycles.
Surface Friction
The surface roughness controls the friction coefficient against the ball, allowing for predictable spin rate generation.
Operating Conditions That Break Cheap Alternatives
A line that stops twice a month rarely blames the part but rather the thermal degradation of the handle-to-head interface. Cheap alternatives utilize standard injection-molded handles that warp when exposed to temperatures exceeding 45°C in direct sunlight. This thermal expansion creates a mismatch in the mating fit, leading to catastrophic joint failure under lateral torque.
UV exposure also acts as a primary failure mode for "funny" designs. Without a UV-stabilized clear coat, the pigments undergo oxidation and delaminate within 50 hours of solar exposure. We specify a multi-layer process to ensure the pigment remains chemically bonded to the carbon fibers.
Production Route and Its Effect on Tolerances
CNC machining of the honeycomb core ensures a perfectly flat mating surface that manual cutting cannot achieve. This precision is vital for maintaining a consistent weight-balance variance of +/- 3 grams across the entire production run.
| Parameter | Range | Tolerance Limit |
|---|---|---|
| Total Face Thickness | 11mm - 16mm | ±0.1mm |
| Core Density | 30 - 40 kg/m³ | ±2% |
| Overall Weight Variance | 190g - 230g | ±3g |
Customisation Boundaries and Tooling Implications
Customizing the geometry requires new steel molds for the handle injection process. While surface-level designs are flexible via digital printing, the structural tooling cost scales with the complexity of the aerodynamic profile. We recommend standardized edge profiles to minimize lead-time for custom graphic orders.
| Customization Type | Technical Constraint | Production Impact |
|---|---|---|
| Graphic Overlay | Substrate Adhesion | Low (Digital UV) |
| Handle Geometry | Mold Cavity | High (New Tooling) |
| Core Material | Structural Integrity | Medium (Sourcing) |
Sector-Specific Installation Notes
Retail-ready assembly focuses on the grip-wrap's moisture resistance. Using a polyurethane-based grip requires a specific curing-time on the handle to prevent slippage in high-humidity environments. For tournament-grade specifications, we focus on the balance-point calibration, measuring from the heel-edge to ensure performance consistency across the batch.
What Gets Measured Before Shipment
- Static load testing of the face-core bond to verify adhesive-shear resistance.
- Weight-distribution mapping to identify center-of-gravity offsets.
- Surface hardness testing (Shore D) on the printed layers to ensure wear resistance.
- Dimensional verification of the edge perimeter using digital calipers for aerodynamic profile compliance.
Questions Buyers Ask Before Ordering
What is the minimum order for custom UV-printed designs?
The MOQ is typically 500 units per design to offset the cost of the UV-ink setup and color-calibration cycles.
Can you provide CAD files for handle modification?
We accept .STEP or .IGES files with a minimum wall thickness of 2.5mm to ensure structural stability during injection molding.
Ready to optimize your production line?
Request an engineering consultation



