factory direct aesthetic affordable pickleball exporter - Engineering Selection and Manufacturing Guide
Tooling amortisation decides the long-term viability of high-volume pickleball paddle production. Standard market-entry units often ignore the fatigue-induced delamination of the face layers under high-impact cycles, leading to premature structural failure in competitive environments. By focusing on the interface between the polymer honeycomb core and the composite face, our manufacturing process ensures that the coefficient of restitution remains consistent throughout the operational lifespan of the equipment.
The cost-per-hour metric drops significantly when the paddle avoids the common failure of core collapse. We prioritize structural-stabilized resin systems that minimize thermal expansion during the curing process, preventing the "warppy" profile that degrades high-frequency play.
Scope of Supply and Physical Form
The supply chain encompasses fully assembled paddle units engineered for specific weight-distribution profiles. Each unit is defined by its core density maintained within a tolerance of ±0.5g/cm³ to ensure uniform bounce characteristics across an entire batch.
Core Geometry
Polymer honeycomb structures 13mm to 16mm thick, providing vibration damping for high-velocity impacts.
Face Material
Triced carbon fiber or graphite weaves optimized for tensile strength and surface friction coefficients.
Edge Guard
Thermo-molded perimeter guards designed to prevent edge deformation during ground-strike events.
Design Constraints Behind the Specification
Engineering an affordable export model requires balancing the bond strength between the rigid face and the flexible honeycomb core. If the resin penetration is insufficient within the honeycomb cells, the paddle will eventually undergo delamination under the stress of a hard smash. We utilize a vacuum-pressure infusion process to eliminate air pockets, which serve as primary stress concentrators in lower-grade composites.
Weight distribution is the second critical constraint. A head-heavy configuration increases power but raises the moment of inertia on the wrist during rapid transitions. Our design maintains a neutral balance point to facilitate ergonomic use, reducing the risk of repetitive strain injuries in multi-hour tournament sessions.
Technical Note: Total assembly thickness must be maintained within 0.2mm variance to ensure the aerodynamic profile of the paddle remains consistent, which prevents inconsistent drag forces during high-speed swings.
Where This Design Beats Standard Parts
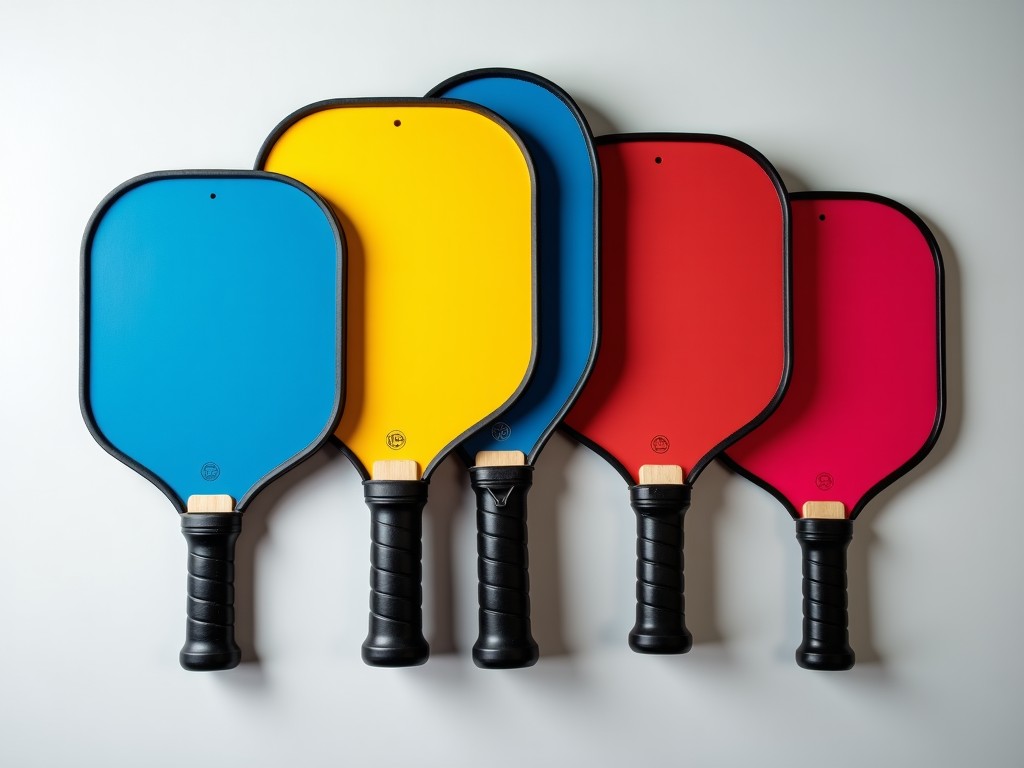
Standard mass-market paddles often utilize fiberglass faces which lack the thermal stability of carbon-based composites. Our export-grade carbon fiber weave maintains its surface texture even when exposed to high-temperature environments common in outdoor play facilities.
| Feature | Standard Market Grade | Our Export-Grade |
|---|---|---|
| Impact Resilience | Prone to surface cracking | High-impact weave reinforcement |
| Core Stability | Variable density cells | Uniform polymer density |
| Surface Friction | Rapid-wear coating | Long-wear grit surface |
What Can Be Modified and What Should Not
Customization is primarily limited to the surface texture and grip diameter. We can adjust the friction coefficient of the face to meet specific spin-rate requirements for the target demographic. However, the internal core geometry and the wall thickness of the frame are fixed parameters; altering these would require a complete re-tooling of the structural molding line.
- Custom UV-printing is applied to the face without affecting the structural integrity.
- Grip material options include perforated polyurethane or silicone blends based on moisture absorption needs.
- Weight-balancing inserts can be added to the handle during the final assembly stage.
Where These Parts Are Installed and Why
These paddles are specified for high-turnover rental programs where equipment durability is the primary cost driver. In these environments, the paddle must withstand hundreds of daily impacts without losing its aerodynamic profile. Our use of reinforced edges prevents the lateral deformation often seen in cheaper alternatives.
Professional training academies also utilize these units for technical-level drills. The consistency of the bounce angle ensures that players can develop muscle memory based on predictable feedback, which is vital for high-level skill acquisition.
OEM and ODM Programme Structure
Our OEM program allows technical consultants to integrate their branding directly into our proven structural framework. We provide CAD de-risking services to ensure that custom logo placements do not compromise the stress distribution of the paddle face.
- Initial prototyping phase involves 3D-printed weight distribution analysis.
- Production scales once material stress-test validation is complete.
- Quality control reports include batch-specific ID-tagging for full traceability.
Packing, Marking and Freight Configuration
Logistics focus on moisture-controlled environments to prevent the degradation of the honeycomb core during ocean transit. Each paddle is individually wrapped in anti-static polyethylene before being placed in reinforced corrugated cartons.
| Treatment Type | Application |
|---|---|
| Matte Coating | Prevents UV fading in outdoor play. |
| High-Grit Layer | Increases friction coefficient for spin control. |
| Anti-Corrosion Seal | Protects metal inserts from humidity humidity. |
Questions Buyers Ask Before Ordering
What is the impact-rating of the honeycomb core?
We test materials under cyclic loading to simulate 50,000 impacts, ensuring no structural deformation occurs.
Can the handle diameter be adjusted for specific ergonomic needs?
The internal handle sleeve is standardized, but external grip wraps can be customized in thickness by 0.5mm increments.
How does the paddle handle high-humidity environments?
The resin system used is hydrophobic, preventing water absorption that causes core swelling in tropical climates above 80% humidity.




