Oem Padel Racket Control And Power Company
An OEM padel racket intended for competitive play must balance two opposing performance axes: control, which depends on precise ball placement and vibration damping, and power, which derives from
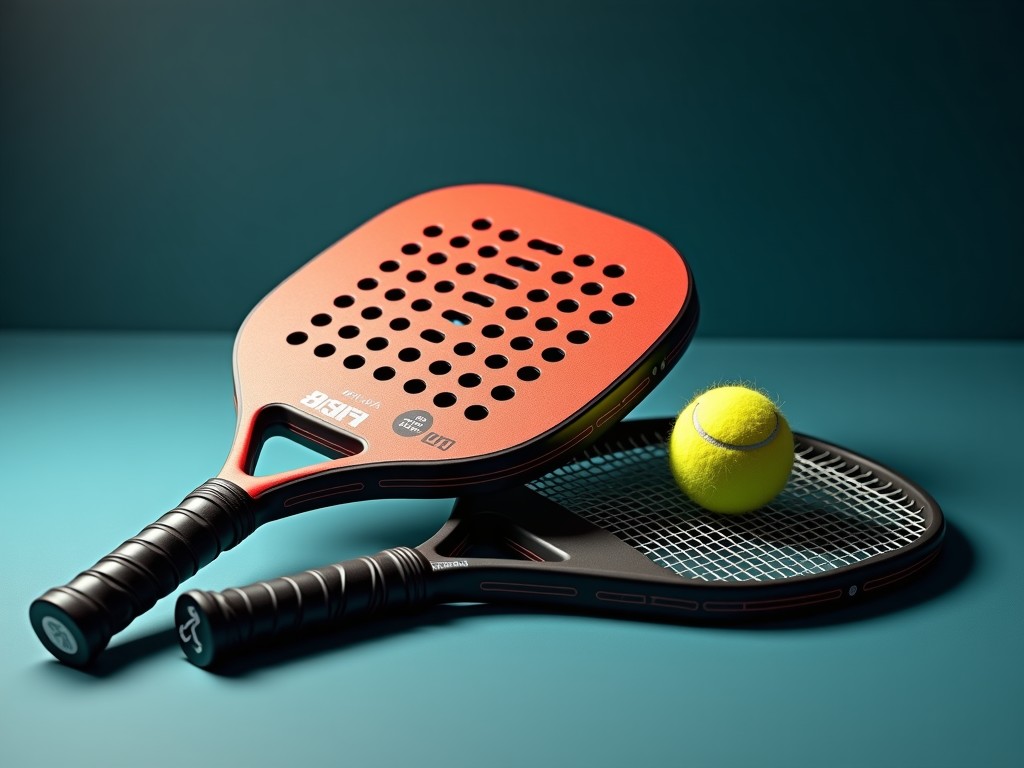
OEM Padel Racket Design for Control and Power
An OEM padel racket intended for competitive play must balance two opposing performance axes: control, which depends on precise ball placement and vibration damping, and power, which derives from stored elastic energy and efficient energy transfer. The following sections detail the engineering parameters that influence each axis and how they can be tuned for specific player profiles.
Frame Geometry and Material Composition
The racket frame is typically manufactured from a unidirectional carbon‑fiber prepreg lay‑up with a nominal fiber volume fraction of 60 %. The lay‑up schedule varies the ply angle from 0° at the throat to ±45° toward the hoop to achieve a target flexural stiffness of 180–220 N·mm² measured at the 3 and 9 o’clock positions. Wall thickness is tapered from 2.2 mm at the throat to 1.6 mm at the tip, reducing mass while preserving torsional rigidity above 2.5 kN·m/rad.
A secondary reinforcement of aramid fibers (0.15 mm thick) is placed at the 12 o’clock position to limit hoop deformation during high‑speed impacts, which otherwise would increase the effective string bed size and reduce control. The resulting frame exhibits a natural frequency of 1150 Hz (±30 Hz) in the first bending mode, a value correlated with perceived “solidity” by players.
Core Construction and Damping Characteristics
The core is injected with a propylene‑based ethylene‑vinyl acetate (EVA) blend whose Shore A hardness can be selected from 35 to 55. Lower hardness (35 – 40) yields a higher coefficient of restitution (≈0.55) favoring power, while higher hardness (50 – 55) reduces restitution to ≈0.48 and increases energy dissipation, improving control. The core density ranges from 0.12 g/cm³ (soft) to 0.18 g/cm³ (firm).
Internal damping is further tuned by incorporating 2 wt % of silicon‑based microspheres that act as micro‑cavities, raising the loss factor from 0.02 (baseline) to 0.045 across the 100 – 500 Hz band. This adjustment reduces peak vibration amplitude at the handle by approximately 30 % measured with a laser vibrometer under a 30 m/s impact simulation.
String Pattern and Tension Influence on Control vs Power
The string bed uses a 16 × 19 pattern (main × cross) with a nominal string diameter of 1.25 mm (polyester). Varying the main‑to‑cross ratio from 16 × 19 to 14 × 21 changes the effective string bed stiffness by ±12 %, which directly influences the launch angle distribution. A tighter pattern (more crosses) yields a narrower launch angle spread (±3°) beneficial for control, whereas a more open pattern increases spread to ±5°, enhancing power potential.
Recommended tension range is 22 – 28 lb (10 – 12.5 kg). At 22 lb the string bed exhibits a deflection of 4.2 mm under a 150 N load, storing ≈0.35 J of elastic energy; at 28 lb deflection drops to 3.1 mm with stored energy ≈0.26 J. Players seeking higher power typically select the lower end of the tension range, while those prioritizing control opt for higher tension.
Weight Distribution, Balance Point, and Swing Weight
Total racket mass is adjustable between 340 g and 380 g in 5 g increments by altering the amount of carbon‑fiber reinforcement in the throat and tip zones. The balance point (distance from butt end to center of mass) can be set from 260 mm (head‑light) to 290 mm (even balance) in 2 mm steps. Swing weight, calculated as the integral of mass × radius² about the butt, ranges from 260 kg·cm² (head‑light) to 290 kg·cm² (even balance).
A head‑light configuration (balance ≤ 270 mm, swing weight ≤ 270 kg·cm²) reduces rotational inertia, facilitating quicker wrist action and improved control on volleys. An even‑balance configuration (balance ≈ 285‑290 mm, swing weight ≈ 285‑290 kg·cm²) raises stored rotational energy, translating to higher ball speed on groundstrokes.
Customization Options
- Frame modulus: 70 GPa (standard carbon) or 80 GPa (high‑modulus carbon) – affects stiffness and weight.
- Core hardness: Shore A 35‑55 in 5‑point increments – tunes power/control trade‑off.
- Balance point: 260‑290 mm (2 mm steps) – adjusts swing feel.
- Total mass: 340‑380 g (5 g steps) – influences maneuverability.
- Grip size: 4 in, 4¼ in, 4½ in (circumference) – accommodates hand dimensions.
- String pattern: 16×19, 14×21, 16×18 – modifies launch angle distribution.
Typical Performance Ranges
| Parameter | Minimum | Typical | Maximum |
|---|---|---|---|
| Frame stiffness (N·mm²) | 180 | 200 | 220 |
| Core hardness (Shore A) | 35 | 45 | 55 |
| Total mass (g) | 340 | 360 | 380 |
| Balance point (mm from butt) | 260 | 275 | 290 |
| Swing weight (kg·cm²) | 260 | 275 | 290 |
| String tension (lb) | 22 | 25 | 28 |
Applications in Competitive and Training Environments
Rackets tuned toward the lower mass, head‑light end of the spectrum (≈340 g, balance ≈ 260 mm) are favored by defensive specialists who rely on rapid volley exchanges and precise placement near the wall. The reduced swing weight enables faster reaction times, and the higher core hardness provides the damping needed to absorb high‑speed balls without excessive rebound.
Conversely, aggressive baseliners often select configurations near the upper mass and even‑balance limits (≈380 g, balance ≈ 290 mm). The increased swing weight stores greater rotational kinetic energy, translating to higher ball speeds on drives and smashes. A softer core (Shore A ≈ 35) combined with lower string tension maximizes the coefficient of restitution, benefiting power‑oriented play.
Training facilities benefit from offering a matrix of rackets across the customization matrix, allowing coaches to isolate the effect of individual parameters (e.g., varying only balance while holding mass constant) during skill‑development drills.
Quality Assurance and Testing Procedures
Each production lot undergoes three‑point bend testing on the frame to verify flexural stiffness within ±5 % of the target value. Impact testing is performed with a pneumatic ball launcher at 30 m/s, measuring rebound velocity and vibration acceleration at the handle using a triaxial accelerometer; acceptance criteria are rebound velocity variance < 3 % and peak handle acceleration < 15 g.
Mass and balance are verified on a calibrated scale and a precision balance beam with resolution of 0.1 g and 0.5 mm respectively. String tension is checked with a digital tension meter after stringing, ensuring the set point is within ±0.5 lb. All inspections are documented in a traceable batch record linked to the serial number etched on the throat.
Packaging and Logistics for OEM Delivery
Rackets are packed in individual corrugated cardboard sleeves with interior polyethylene foam inserts that limit axial compression to < 0.2 mm and prevent surface abrasion. Six sleeves are placed in a master carton of dimensions 380 mm × 260 mm × 120 mm, achieving a gross weight of ≤ 2.4 kg. Cartons are strapped with polypropylene bands and labeled with handling symbols indicating “Keep Dry” and “This Side Up”.
For sea freight, cartons are stacked on pallets with a maximum load of 800 kg, protected by a top and bottom layer of corrugated divider sheets. Air shipments utilize lightweight plywood crates with internal bracing to resist acceleration forces up to 2 g. All packaging materials meet ISPM‑15 standards for international transport.
Frequently Asked Questions
Can the frame geometry be adjusted for a specific player’s swing style?
Yes. The lay‑up schedule, wall thickness taper, and reinforcement placement are all modifiable via the tooling program. Adjustments are quantified by changes in flexural stiffness (±10 %) and torsional rigidity (±8 %).
What information is required before a quotation can be issued?
We need the target mass range, desired balance point, core hardness preference, string pattern, and grip size. If the customer wishes to specify a particular carbon‑fiber modulus or aramid reinforcement layout, those details should be included as well.
How is quality inspected for each batch?
Every lot receives flexural stiffness, impact rebound, vibration, mass, balance, and string‑tension checks as described in the Quality Assurance section. Results are recorded and available upon request.
What packaging methods are available for OEM orders?
Standard packaging includes individual foam‑sleeved cartons as described. Optional upgrades are available: moisture‑barrier bags, custom‑printed cartons, or palletized configurations with corner protectors.
Ready to Discuss Your OEM Requirements?
Our engineering team can translate your performance targets into a detailed racket specification, including lay‑up schedule, core formulation, and tolerance limits. To begin a technical conversation, please use the link below.
Request Technical Specification Sheet



