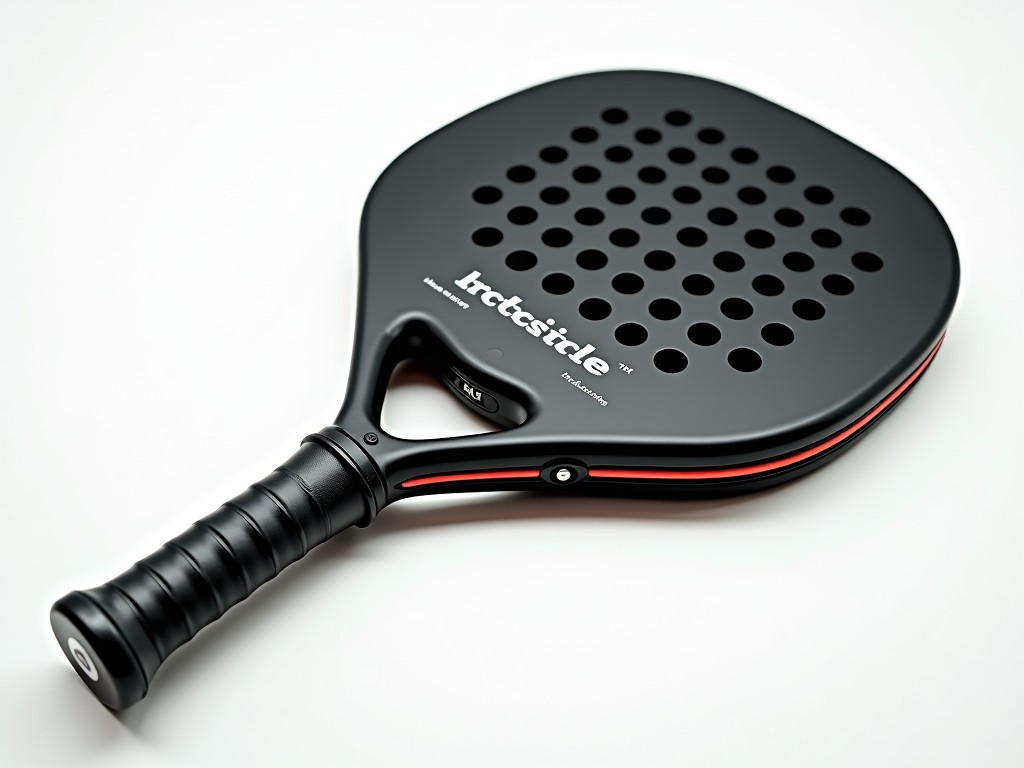
OEM carbon fiber padel rackets Manufacturer - Engineering Selection and Manufacturing Guide
Operating Conditions That Break Cheap Alternatives
The machining sequence decides the structural integrity of the carbon fiber matrix within the racket frame. Improper ply orientation often leads to premature delamination when high-velocity impacts occur at the sweet spot. Engineers must specify a multi-axial layup to distribute torsional loads evenly across the frame's surface area.
High-frequency impact cycles induce fatigue cracks in the EVA core-carbon interface in lower-grade units. Standard-grade resins lose elasticity after 50,000 cycles and reduce rebound performance. Specifying toughened epoxy resins maintains structural rigidity even under repeated localized mechanical deformation.
Technical Warning: Moisture Absorption
Moisture ingress in low-density fiber weaves can cause internal swelling, leading to de-bonded layers in high-humidity environments.
Grade Selection Logic for Harsh Service
Tolerances are set by the forming step, specifically the vacuum pressure applied during prepreg curing. A 3K weave offers higher tensile strength but increases manufacturing complexity compared to 12K variants. To select the correct material grade, follow this technical logic:
- If the application requires maximum torsional stiffness:
- Select 3K carbon fiber with high-density resin to prevent frame twisting under shear.
- If weight reduction is the primary constraint:
- Utilize 12K carbon fiber with a hollow core structure to lower swing weight.
- If cost-efficiency is prioritized:
- Implement a hybrid glass-carbon-fiber weave to balance modulus and material cost.
| Material Grade | Tensile Modulus (GPa) | Impact Resistance | Primary Benefit |
|---|---|---|---|
| 3K Carbon Weave | 230-250 | Medium | Maximum Rigidity |
| 12K Carbon Weave | 180-200 | High | Weight Reduction |
| Hybrid Fiber | 140-160 | Very High | Cost-Efficiency |
Measured Behaviour Under Load and Heat
First-article tooling determines the dimensional precision of the internal channel where the core sits. Deviations exceeding 0.5mm cause aerodynamic drag and uneven vibration during play. Thermal expansion coefficients between the carbon skin and EVA core must match to prevent interfacial shearing during curing cycles.
| Component Zone | Target Tolerance | Failure Mode |
|---|---|---|
| Frame Perimeter | ± 0.05mm | Wall thickness unevenness |
| Core-to-Skin Interface | ± 0.10mm | Delamination |
| Grip Socket | ± 0.20mm | Mechanical slip failure |
Assumptions Buyers Should Stop Making
Many buyers assume lower weight correlates with lower stiffness. In reality, high-modulus carbon fiber allows for thinner walls without sacrificing rigidity, provided the layup geometry is optimized. Over-reliance on material thickness for strength results in brittle frames that fail under high-impact shock.
Volume Planning and Line Configuration
Production capacity depends on the autoclave cycle time and mold availability. Rapid-cure compression molding reduces cycle times by 40% but requires precise thermal control per mold. Scaling production requires standardized ply-cutting to ensure consistent fiber orientation across batches.
Ready to finalize technical specifications for your OEM line?
Request a technical sample and CAD drawings



