Specifying direct factory white padel racket and balls exporter for Industrial Service
How the Geometry Handles Load and Sealing
| Parameter | Technical Range | Industrial Benefit |
|---|---|---|
| Core EVA Density | 500 - 650 kg/m³ | Energy absorption vs. power return |
| Frame Thickness | 23mm - 38mm | Torsional rigidity under offset loads |
| Ball Pressure | 9.5 - 11.5 PSI | Flight trajectory consistency across thermal gradients |
Structural integrity in padel rackets depends on the distribution of kinetic energy during high-velocity impacts. A reinforced perimeter geometry mitigates stress concentration at the bridge area, which prevents premature delamination of the carbon-fiber-foam interface.
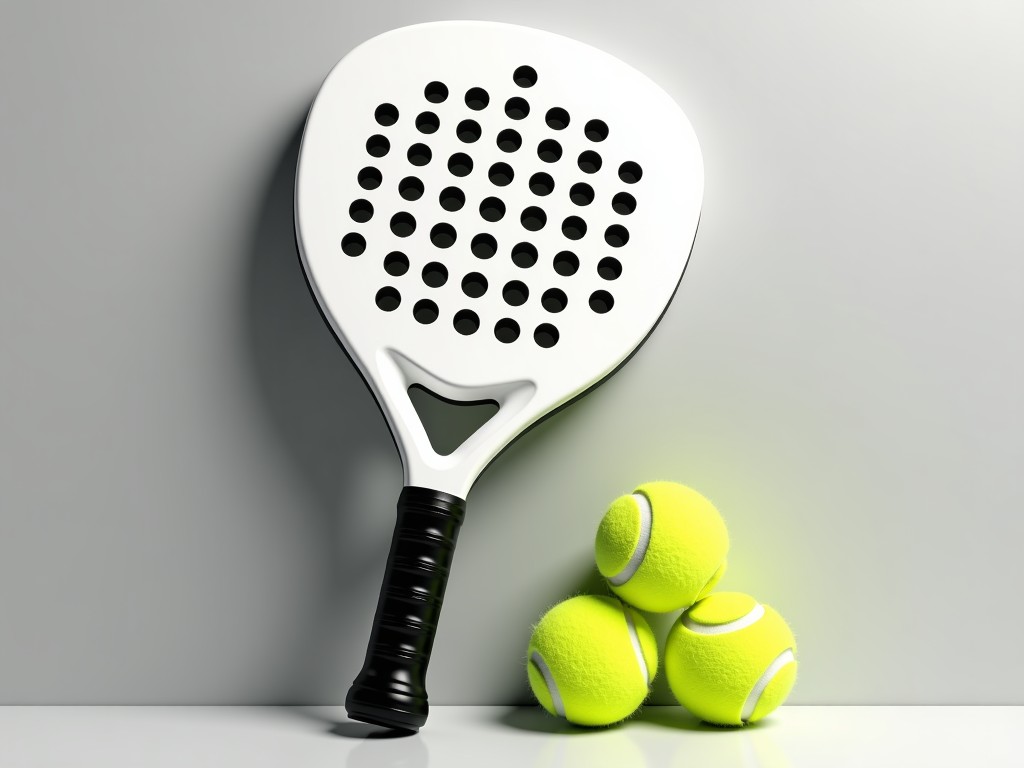
The white-finish coating requires UV-stabilized polymers to prevent yellowing in outdoor court environments. This ensures the aesthetic specification matches the technical performance requirements even after prolonged exposure to solar radiation.
Material Grades and Their Trade-offs
Material selection dictates the fatigue life of the equipment. While higher-thread-count carbon weaves offer increased stiffness, they increase the risk of brittle failure if the racket experiences localized impact shockloads.
12K Carbon Fiber
The 12K weave provides a wider fiber pattern, resulting in a larger elastic zone. This flexibility reduces vibration for players who prioritize joint protection but limits maximum output compared to denser weaves.
3K Carbon Fiber
A denser 3K weave maximizes surface hardness and response speed. It is ideal for high-performance applications where immediate energy transfer is the primary metric of mechanical success.
Ball manufacturing utilizes--grade rubber blends to maintain internal pressure. Standard-grade elastomers often undergo permanent deformation after three match cycles, leading to inconsistent bounce heights that undermine competitive play.
Forming, Machining and Joining Steps
The production cycle begins with vacuum infusion of resin into pre-pregnated carbon layers. This process minimizes air-void formation within the laminate, which serves as the primary initiation point for structural failure in composite-based sports equipment.
Post-machining involves CNC-drilling aerodynamic hole patterns. These holes must be deburred to prevent micro-cracks that could otherwise propagate through the frame under repeated cyclic loading.
What Can Be Modified and What Should Not
OEM clients can customize the surface roughness, ranging from smooth-finish to grit-like textures. This modification affects the friction coefficient during ball contact without altering the structural properties of the core.
The internal core density is a non-modifiable parameter. Altering the foam density post-design would require a complete recalibration of the racket's balance point and swing weight metrics.
What Gets Measured Before Shipment
Every batch undergoes a standardized bounce test to verify the elastic modulus of the EVA core. Deviations beyond a 5% tolerance trigger a rejection of the unit to ensure fleet performance consistency.
- Weight balance within +/- 2 grams of the target specification.
- Internal ball pressure variance within +/- 0.5 PSI.
- Surface coating adhesion via cross-tape test.
Keeping the Line Fed Across Seasons
Direct factory sourcing allows for buffer stocking of raw carbon fiber and rubber compounds. Maintaining a three-month raw material inventory mitigates risks associated with global shipping fluctuations and seasonal demand.
Questions Buyers Ask Before Ordering
How does the white finish affect the thermal absorption?
The white pigment provides a higher albedo compared to dark frames, which prevents the internal core from softening during play in direct sunlight.
What is the lead time for custom mold tooling?
Initial tooling typically requires 45 to 60 days for CNC-machined aluminum molds before the first production run.




